Precision processing capability
A wide range of tolerance options to ISO 2768 (standard and fine grade) and ISO 286 (grades 8, 7, 6).
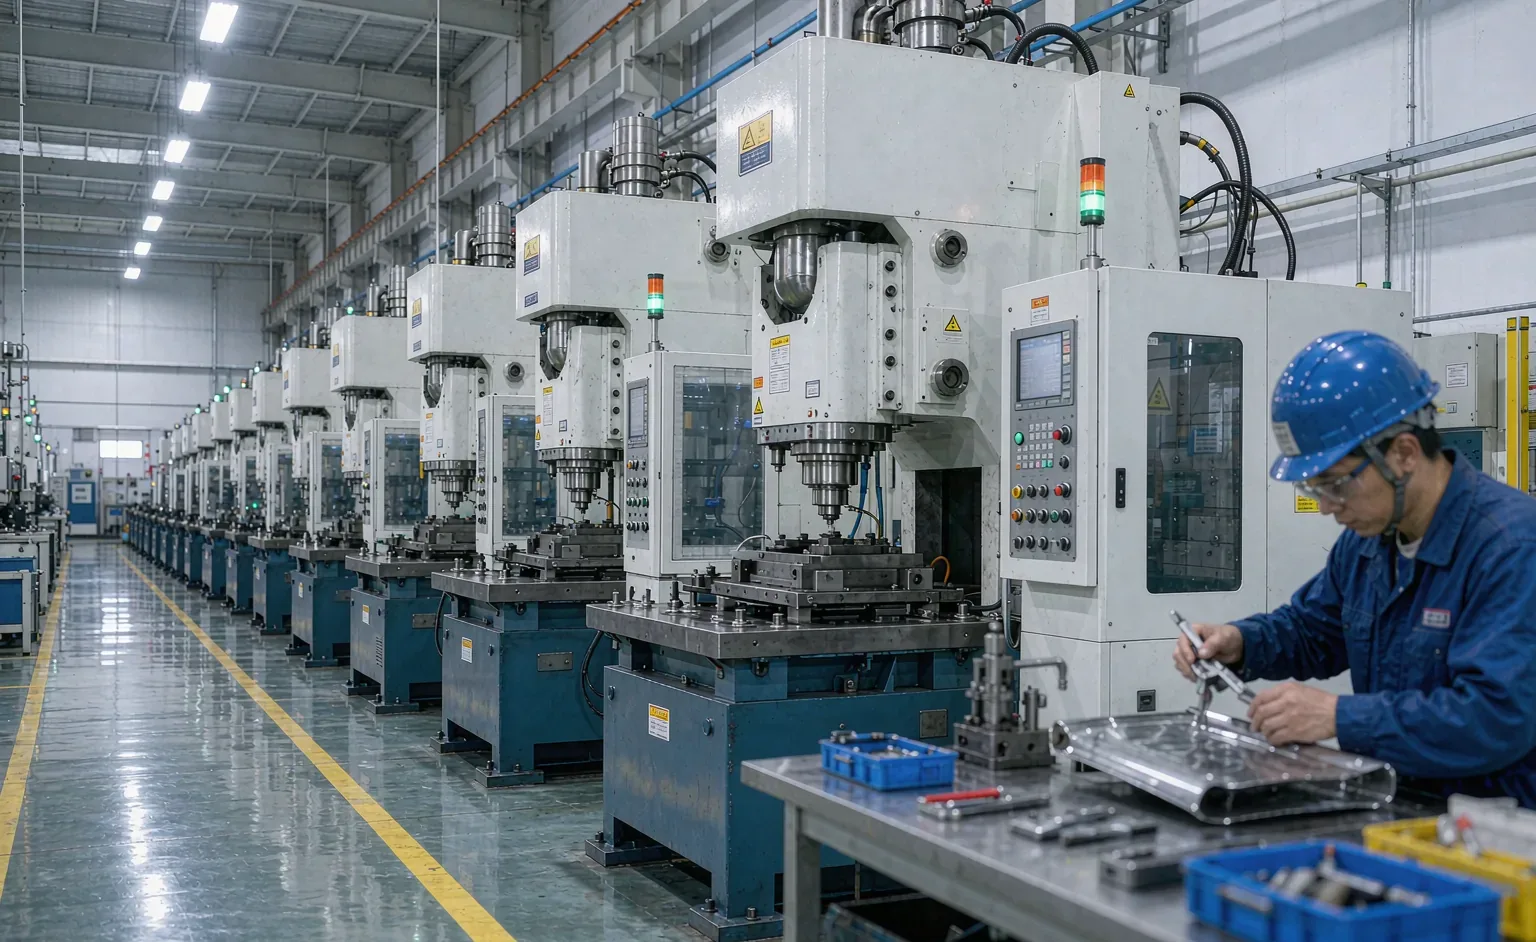
Single-cavity, progressive and compound dies from 25 to 400 tonnes, holding ±0.05mm repeatability across high-volume flat and shallow parts. Over 5,000 dies in house and an 18-minute changeover keep schedule pressure off your programme — supporting flexible switching between 50–5,000 piece multi-variety runs and over 100,000 piece volumes.
Most of these are coordination failures rather than manufacturing problems. Here is how each one is handled here.
Professional analysis, evaluation and verification of manufacturing feasibility before tooling.
No need for professional engineering 3D drawings. A sketch with dimensions is enough to start.
Strict quality management with 100% inspection from raw material through to finished goods.
Specialised personnel, specialised service, specialised quotation. Reply within 2 working hours.
Information-based production management with controllable, visible progress.
From prototype design development through prototyping and batch production, we provide materials, finishes and a complete process flow in one order.
Tooling design, cutting, assembly and hardening carried out in our own die shop.
02High-speed disc blanking from coil with decoiling and levelling.
03Pierce, form and cut in a single stroke for high-volume flat parts.
04Two-level forming where the part geometry demands it.
05Edge breaking so stacked parts do not scratch each other.
06Press and rivet fasteners; peening for permanent attachment.
07Zinc, nickel and tin plating, or powder coat, on stamped surfaces.
08Part of the complete precision stamping process flow, handled in-house.
10,000m² facility with over 100 machines across cutting, forming, joining and inspection — all under one roof, all calibrated and traceable.
Progressive and compound die setups with automatic oiling and part ejection.
PRESS LINECoil-to-blank line with decoiling, straightening and levelling for consistent material.
COIL LINEDesign, cutting, assembly, hardening and maintenance of 5,000+ stamping dies in-house.
DIE SHOPDie inspection and relief cutting to keep dimensions stable across die life.
DIE SPOTTINGPayload feeders, transfer feeds and vibratory bowl feeding for stable line rate.
FEEDINGHeat number and part marking for full batch traceability on stamped parts.
MARKINGEvery new die verified on the CMM before batch production starts.
INSPECTIONWe provide selection advice based on your application, then recommend the configuration that gets you the best cost and performance balance.
Excellent strength-to-weight ratio, high thermal and electrical conductivity, low density and natural corrosion resistance. Can be anodized.
Corrosion resistance and strength at temperature. Food-safe, medical and outdoor grades available.
The lowest-cost structural option. Best for brackets, frames and enclosures where cosmetic finish is secondary.
High electrical and thermal conductivity with natural corrosion resistance. Machines cleanly for connectors.
Six times stronger than aluminium at half the weight of steel. Aerospace, medical and marine grades.
Hardened tooling and wear components. Also supplied as spare die parts machined from these grades.
A common thermoplastic with excellent impact resistance, thermal stability and chemical resistance. Easy to machine, smooth surface finish.
High impact strength with a Class V flame rating. The default for consumer electronics housings.
Low friction and wear resistant. Used for gears, bushings and sliders; glass-filled grades add stiffness.
Dimensional stability and low friction. Excellent for precision gears and snap-fit features.
Continuous 250°C service temperature with chemical and wear resistance. Medical and aerospace.
Non-stick, chemically inert and very low friction. Seals, gaskets and insulator components.
Thousands of finished part case studies. Send a drawing and we will show you comparable parts we have already made.
Full-chain autonomous control — which is what makes the quality-price ratio work.
A wide range of tolerance options to ISO 2768 (standard and fine grade) and ISO 286 (grades 8, 7, 6).
Over 100 sets of equipment and a fully self-contained team complete high-precision prototypes within hours.
100% inspection from raw material through semi-finished to finished goods, under ISO 9001 management.
Sheet metal parts coordinated with CNC and EDM through information management, reducing cost and lead time.
A dedicated business manager, engineer and support team giving 1+1+N project-based service.
Anodizing, electroplating, powder coating and painting to enhance durability and appearance.
Choose us, and ensure every processed item is durable and visually appealing.
Email it to pengfeng@pf898.com, or describe the part in the quote form.
Engineer reviews manufacturability. Reply within 2 hours.
Tooling starts on confirmation; batch tracked to your schedule.
In-process SPC plus final CMM measurement and written report.
Export packing, documents and door-to-door delivery.
Cost is material plus tooling (if any) plus processing time plus finishing, quoted as one line-item breakdown. Tooling is a one-off; repeat orders in the same part drop to the unit price alone.
Prototypes take 3–5 days. Standard production is 7–15 days depending on volume and finishing. Anodizing and powder coating add 2–4 days because they are batch processes.
Any batch failing our own acceptance criteria is replaced or reworked at our expense before it ships. Every shipment carries a dimensional report and material certificates.
Yes. We sign mutual NDAs before file review and will hold tooling exclusively for your part with your name stamped on it.
STEP, STP, DWG, DXF, IGES, IGS, PDF, and images. A sketch with the key dimensions and tolerance is enough to start — engineering drawings are not required.
Any batch that fails our own acceptance criteria is replaced or reworked at our expense before it ships — not after you complain. Every order carries a dimensional report and EN10204 3.1 material certificates as standard.